Detroit, Michigan SYSTEM ONLINE

Building the logic that runs
the assembly line.

I'm an Industrial Engineering student at Wayne State University and an automation engineer who programs the PLCs, HMIs, and inspection systems that keep automotive production lines running — and catches the failures that shouldn't reach the next station.

2+ Years of hands-on PLC, HMI & vision commissioning
Focus
Automation & controls
Program
B.S. Industrial Engineering, exp. 2027
Certifications
Six Sigma Green Belt GCCH-1 GCCS-2

Experience

Three roles, three different floors — a control room, a courtside, and a lumber yard.

  1. Jan 2023 – Aug 2023  ·  May 2024 – May 2025  ·  May 2026 – Aug 2026

    Automation Engineer

    Control System Integrators — Lansing, MI

    • Programmed PLC logic and HMIs for automotive-industry projects with customers including GM Toledo and GM LDT.
    • Built new inspection logic for a camera system at GM Lansing Delta Township to raise failure detection on final vehicle assembly.
    • Commissioned the AMR traffic system at GM Toledo, coordinating autonomous mobile robots that transport transmissions through truck and van manufacturing.
    Studio 5000 TIA Portal FTView PLC / HMI
  2. Aug 2019 – Oct 2019

    Boys Freshman JV Tennis Coach

    Northville High School — Northville, MI

    • Coached a freshman tennis team through practices and matches against nearby schools.
    • Led practices as lead instructor and built a team-first culture for first-year players.
  3. May 2021 – Jun 2021

    Forklift Driver

    Guthrie Lumber Company — Livonia, MI

    • Packaged customer orders for delivery trucks and kept the yard organized.
    • Operated a forklift to fill orders on time and keep material moving to schedule.

Education

Wayne State University

Bachelor of Science, Industrial Engineering

Expected graduation: May 2027

Completed coursework

  • Quality Control
  • Engineering Economy
  • Work Design
  • Six Sigma
  • Systems Simulation

Current coursework

  • Engineering Capstone
  • Digital Automation
  • Operations Research
  • Data Science & Analysis
  • Systems Engineering

Skills

Programming

  • Python
  • MATLAB
  • C++

Controls & automation

  • Studio 5000
  • TIA Portal
  • FTView

Certifications

  • Six Sigma Green Belt
  • GCCH-1
  • GCCS-2

About Me

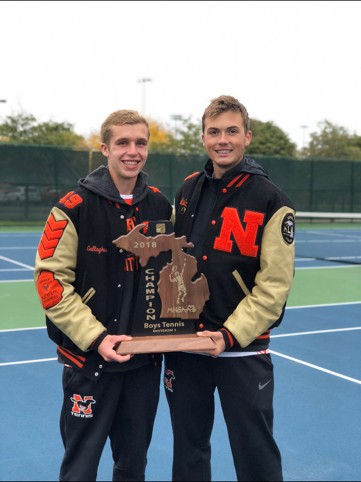
Ilija and a teammate holding the 2018 Michigan Division 1 boys tennis championship trophy

I love to get outside and play tennis or basketball. I also am an avid reader and like to catch a local play or musical. I also like board games like Settlers of Catan and getting together with family.

Dual Laser Architecture & Industrial Controls

xTool F1 Ultra 20W Laser Engraver

A technical guide to the premier 20W Fiber and 20W Blue Diode dual-source galvo workstation. Review the fundamental physics of laser energy below, inspect the engineering classification, and explore the interactive SOP chapters.

Laser Technology Primer

How Lasers Work & Revolutionized Modern Manufacturing

1. What Is a Laser & How Does It Work? Laser Physics Principle"Light Amplification by Stimulated Emission of Radiation." Monochromatic, coherent photons focused through optical resonator mirrors.

Ordinary light bulbs produce a chaotic blend of all colors scattered in every direction. A laser synchronizes every photon so they share the exact same wavelength and oscillate in perfect unison. Inside a mirrored optical cavity, excited atoms release identical bursts of light that multiply in intensity before escaping through a precision focal lens.

2. How Lasers Became Industrial Workhorses Manufacturing History: 1960–1970sFirst developed in 1960. Early industrial adoption focused on drilling diamond wire dies, cutting structural sheet alloys, and eliminating mechanical tool wear.

Invented in 1960 and originally called "a solution looking for a problem," manufacturing engineers quickly realized focused light never dulls, exerts zero physical tool drag on fragile workpieces, and slices intricate geometries without mechanical stamping dies or tool replacement downtime.

3. Three Dominant Industrial Laser Types Optical Absorption SpectraFiber (~1064 nm) for metals; Diode (~445–455 nm) for organics/woods; CO₂ (~10,600 nm) for transparent acrylic and glass.

  • Fiber Lasers (~1064 nm Infrared): Generated inside rare-earth doped optical fibers. Highly absorbed by bare metals (steel, aluminum, brass) and dense plastics. Standard for automotive serialization.
  • Diode / Blue Lasers (~445–455 nm Visible): Solid-state semiconductor lasers absorbed by organic materials like wood, leather, paper, and dark acrylics.
  • CO2 Lasers (~10,600 nm Far-Infrared): Gas-tube lasers historically dominant for transparent glass, clear acrylics, and thick timber.

4. Gantry vs. Galvanometer (Galvo) Engraving Kinematic Beam SteeringGantry systems move mechanical axes at 200–600 mm/s. Galvanometer mirror scanners deflect light at up to 10,000 mm/s for high-volume automated lines.

  • Gantry Systems: The laser head rides along mechanical rails and timing belts over X and Y axes (like a 3D printer). Good for huge beds, but restricted to moderate speeds (200–600 mm/s).
  • Galvanometer (Galvo) Systems: The laser head stays stationary overhead. Twin high-speed micro-motor mirrors swivel within fractions of a millimeter to steer the beam down at up to 10,000 mm/s for mass production.

5. Equipment Categorization: xTool F1 Ultra 20W Official Machine TaxonomyEnclosed Dual-Source Hybrid Galvanometer Laser Workstation (20W Fiber + 20W Diode, 10,000 mm/s, Class 1/4).

The xTool F1 Ultra is formally categorized as an Enclosed Dual-Source Hybrid Galvanometer Laser Workstation. It combines both Fiber (1064 nm) and Diode (445 nm) oscillators into a single galvo head with automated software switching:

Architecture Dual-Source Galvanometer (Galvo)
Laser Sources 20W Fiber (1064 nm) + 20W Diode (445 nm)
Kinematic Speed 10,000 mm/s Vector Scan
Envelope Class Class 1 (Interlocked) / Class 4 (LOTO Key)
Chapter 01

Core Architecture & Dual Laser Physics

The F1 Ultra combines two industrial-grade laser sources into an ultra-fast galvanometer scanning chassis:

  • Dual 20W Laser Sources: Integrates a 20W 445 ± 15 nm Blue Diode laser and a 20W 1064 ± 5 nm Infrared Fiber laser, switching automatically via software to engrave wood, acrylic, bare metals, and plastics Quick Start Guide: P. 04"Laser module: 445 ± 15 nm blue-light laser (20 W) / 1064 ± 5 nm fiber infrared laser (20 W)." .
  • 10,000 mm/s Galvo Speed: High-speed internal galvanometer mirrors steer the focused beam across a 220 × 220 mm native working area at up to 10,000 mm/s Quick Start Guide: P. 04"Internal working area: 220 mm × 220 mm. Maximum processing speed: 10,000 mm/s." .
  • Safety Classification (Class 1 vs. Class 4): Produced in two models: MXF-K002-001 (Class 1 enclosed system) and MXF-K002-B20 (Class 4 laser system) Quick Start Guide: P. 01 & 04"xTool F1 Ultra comes in two models: MXF-K002-001 (Class 1) and MXF-K002-B20 (Class 4)." .
Chapter 02

Commissioning & Hardware Preparation

Execute this 5-point physical commissioning routine before supplying main 24V–25V DC power:

Step 1

Lens Protector

Pull down the field lens cap to remove it prior to every operational session Quick Start Guide: P. 05"Pull down the field lens protector to remove it... Ensure that the protector is removed every time before you use the machine." .

Step 2

Access Key

Insert the access-control key / interlock connector into the rear bus Quick Start Guide: P. 05"Insert the key. You can remove the key to disable the processing and related functions of the machine." .

Step 3

Release E-Stop

Turn the red E-Stop clockwise to release. Never use it as a power switch Quick Start Guide: P. 05 & 08"Ensure that the emergency stop button is released... Do not use the emergency stop button as a power switch." .

Step 4

Install Pipe

Clamp the flexible exhaust duct onto the rear exhaust outlet Quick Start Guide: P. 06"Install the pipe." Connects directly to smoke outlet or purifier. .

Step 5

Touch Controller

Plug in the touchscreen controller cable with the notch facing up Quick Start Guide: P. 06"To insert the connector, ensure that the notch at the end faces up." .

Chapter 03

Accessories & Workholding Registration

Proper fixture installation ensures optical safety and geometric repeatability:

  • Slatted Panel for Laser Cutting: Install the slatted panel when cutting materials to reduce burning on the underside and protect the baseplate Quick Start Guide: P. 07"To cut a material, you are advised to use the slatted panel. It can reduce the areas burned during material processing and protect the baseplate." .
  • L-Shaped Positioning Piece: Screw the L-shaped bracket directly into baseplate datum holes during batch runs to register materials in the exact position every time Quick Start Guide: P. 07"During batch processing, the L-shaped positioning piece can help you place a material in the same position every time." .
Chapter 04

Touchscreen Controller & Software Workflows

Coordinate standalone machine actions and computer-guided vector jobs:

  1. Use the 3 dedicated physical controller buttons: Up/Down for manual focal lifting, Framing to outline boundaries, and Start/Stop to run jobs Quick Start Guide: P. 04"Up/Down button: Lifts/lowers laser module. Framing button: Starts/stops framing. Start/Stop button: Starts/stops material processing." .
  2. Power on via the side rocker switch and configure UI language on the touchscreen display Quick Start Guide: P. 08"Press the power switch to turn on xTool F1 Ultra... Set up the language of the touchscreen controller." .
  3. Connect via USB-C or Wi-Fi to xTool Creative Space (XCS) to import vector art, select material profiles, and initiate optical autofocus Quick Start Guide: P. 09 & 10"Use software to operate xTool F1 Ultra... connect xTool F1 Ultra in the software." .
Chapter 05

Preventive Maintenance & Optical Hygiene

Optical purity and unrestricted exhaust flow preserve 20W galvo beam intensity:

  • Field Lens Decontamination: If laser power attenuation occurs (shallow engravings or incomplete cuts), clean the field lens with a lint-free cloth moistened with alcohol Quick Start Guide: P. 11"Disconnect power before maintaining... clean it with the lint-free cloth moistened with alcohol." .
  • Exhaust Fan & Smoke Port Cleaning: If smoke escapes the green protective enclosure, clean dust from the internal fan and rear exhaust outlet Quick Start Guide: P. 11"If smoke runs out of the protective enclosure, the fan and smoke outlet may be blocked due to dust. Clean them." .
  • Chassis Tilt Rule: To prevent dust from falling into internal circuit boards during exhaust fan cleaning, slightly tilt the machine back Quick Start Guide: P. 11"To avoid dust falling into the circuit board, slightly tilt the machine." .
Operator Knowledge Verification

xTool F1 Ultra Diagnostic & Safety Assessment

Test everything covered above: laser physics and galvo kinematics, the F1 Ultra's dual-source architecture, commissioning interlocks, workholding accessories, controller workflows, and maintenance procedures. Select an answer to see its explanation.

Technical SOP & Subject Matter Guide

xTool Auto Streamline™ Conveyor

Interactive mechanical integration, precision calibration, batch vision automation, and diagnostics calibrated to the official xTool Quick Start Guide. Review the industrial history of conveyor lines below, check the mechanical classification, and study the operational chapters.

Industrial Engineering Primer

The Evolution of Conveyors: From 18th-Century Grist Mills to Modern Automation

1. Oliver Evans: America's First Automated Mill (1785–1790) Oliver Evans Flour Mill (Delaware)First continuous automated material handling system in world history. Waterwheels powered bucket elevators, screw augers, and flat leather conveyor belts with zero human manual porterage.

Long before Henry Ford, American inventor Oliver Evans designed the world's first fully mechanized factory on Delaware's Red Clay Creek. Evans linked flat leather-and-canvas belt conveyors with vertical bucket elevators and screw augers. Grain entered a ground-floor hopper, ascended via bucket elevators, dried across revolving rake floors, and traveled across continuous flat belts into milling stones—all powered strictly by water wheels without a single manual shovel.

2. Meatpacking "Disassembly Lines" (1870s–1880s) Cincinnati & Chicago Packing HousesOverhead monorail trolley tracks moved animal carcasses past stationary butchering teams. Henry Ford explicitly acknowledged this moving disassembly line as the inspiration for Highland Park.

In Cincinnati ("Porkopolis") and Chicago slaughterhouses, carcasses were hung from overhead trolley hooks and moved continuously along suspended iron rails past stationary butchers. Each worker performed a single repetitive cut. Henry Ford openly credited inspecting these meatpacking disassembly lines as the direct inspiration for reversing the process into an automobile assembly line.

3. Henry Ford's 1913 Highland Park Assembly Line Ford Highland Park Plant (1913)Continuous moving chassis conveyor slashed Model T build time from 12 hours to 93 minutes, establishing core IE concepts of Takt time and continuous flow.

In 1913, Ford introduced the moving chassis assembly line in Michigan. Dragging the car past fixed worker stations cut Model T assembly time from 12 hours down to 93 minutes. This established modern Industrial Engineering: synchronize flow, eliminate transit waste (Muda), and enforce a predictable Takt time across all stations.

4. Industrial Conveyor Geometries & Power Drives Conveyor KinematicsBelt (friction tracking), Roller (box distribution), Pallet (rigid sub-millimeter fixtures), and Overhead (curing/plating). Driven by AC gearmotors or digital closed-loop stepper motors.

  • Belt Conveyors: Continuous friction loops (rubber, PVC, polyurethane) running over slider beds. Best for small-to-medium discrete goods, irregular shapes, and optical camera scanning.
  • Roller Conveyors: Gravity or motor-driven parallel steel cylinders. The backbone of distribution hubs, corrugated box handling, and pallet logistics.
  • Pallet / Transfer Conveyors: Precision rail tracks carrying rigid tooling plates (pallets). Used in automated CNC and robotic cells where parts must register into sub-millimeter coordinates.
  • Overhead Chain/Monorail: Suspended tracks transporting vehicle bodies through dip tanks, robotic weld cells, and paint curing ovens.

5. How Conveyors Are Powered & Controlled Conveyor Power Train & ControlsMotor (AC induction gearmotor or BLDC/stepper) → transmission (timing belt, chain, or direct-drive gearbox) → head roller. Speed governed by VFDs or digital stepper controllers.

  • Drive Motors: Most factory conveyors are driven by AC induction gearmotors (for continuous fixed-speed bulk transfer) or brushless DC / stepper motors (where precise indexing, start/stop positioning, and step-distance calibration are essential).
  • Transmission: Power transfers from the motor drive shaft to the head roller via timing belts, drive chains, or direct-drive gearboxes.
  • Speed & Motion Control: Modern conveyor speeds are governed by Variable Frequency Drives (VFDs) or digital stepper controllers, enabling software to coordinate speed matching, ramp up acceleration smoothly to avoid material slippage, and stop on exact sensor coordinates.

6. Equipment Categorization: xTool Auto Streamline™ Official Conveyor TaxonomyIntegrated Synchronous Flat-Belt Micro-Conveyor with Closed-Loop Stepper Positioning (right-to-left feed, machine vision indexing).

The xTool Auto Streamline™ Conveyor is classified as an Integrated Synchronous Flat-Belt Micro-Conveyor with Closed-Loop Stepper Positioning. It converts a stationary benchtop galvo laser into an automated continuous manufacturing cell:

Conveyor Class Continuous Friction Flat-Belt Micro-Conveyor
Motor & Drive Logic Digital Pulse Stepper Motor / Timed Index
Feed Direction Right-to-Left Longitudinal Travel (P.10)
Process Coordination Overhead Camera Machine Vision (Smart-Fill)
Chapter 01

Safety & Operational Baselines

Operating a continuous auto-streamline conveyor involves strict adherence to optical enclosure thresholds and hand-clearance zones:

  • Enclosure Shield Height (≤ 5 mm): Pull down the protective enclosure until it rests no more than 5 mm above the material before running Quick Start Guide: P. 09 & 10"Pull down the protective enclosure until it remains no more than 5 mm above the material before processing." .
  • E-Stop Unobstructed Reach: Maintain unobstructed physical line-of-sight and immediate reach to the F1 Ultra red emergency stop mushroom button at all times.
  • Active Processing Zone Safety: When placing materials during processing, keep hands away from the central laser processing area to avoid skin injuries Quick Start Guide: P. 09"When placing materials during processing, keep your hand away from the processing area to avoid skin injuries." .
  • Substrate Boundary Rule: Ensure all workpieces are identical and strictly do not touch or overlap with each other on the belt surface Quick Start Guide: P. 09"Ensure that you use identical materials... Ensure that the materials do not touch or overlap with each other." .
Chapter 02

Hardware Docking (F1 Ultra Fastening Kit)

The F1 Ultra utilizes a dedicated fastening kit distinct from the F2 Ultra Quick Start Guide: P. 01"xTool F1 Ultra fastening kit: Fastening piece A, Fastening piece B, Screw M4*10, Screwdriver 3 mm." . Follow the 4-step mechanical docking sequence:

Step 1

Mount Piece B

Fasten Piece B to conveyor using two M4*10 screws and 3 mm driver. Verify correct bracket orientation Quick Start Guide: P. 06"Place fastening piece B in the correct direction. Fastening piece B, Screw M4*10, Screwdriver 3 mm." .

Step 2

Mount Piece A

Attach Piece A to F1 Ultra base plate using two M4*10 screws and 3 mm driver Quick Start Guide: P. 07"xTool F1 Ultra, Fastening piece A, Screw M4*10, Screwdriver 3 mm." .

Step 3

Align & Join

Align the holes on Fastening Pieces A and B; secure together with two M4*10 screws Quick Start Guide: P. 07"Align the holes on the two fastening pieces... Screw M4*10, Screwdriver 3 mm." .

Step 4

Cable Interface

Plug 90° elbow connection cable between conveyor side port and F1 Ultra rear connector Quick Start Guide: P. 08"Connection cable plugged into side of conveyor and peripheral port of F1 Ultra." .

Chapter 03

Software Configuration (XCS)

Synchronize stepper motor index pulses with xTool Creative Space (XCS) to control workpiece progression:

  1. Connect F1 Ultra via USB-C or local Wi-Fi and verify the device dashboard indicates Connected.
  2. Open Device Settings (Gear Icon) adjacent to the F1 Ultra device card in XCS.
  3. Under Working Mode, switch from Regular Surface to Conveyor (select Auto-Stream or Long Material).
  4. Verify software feed vector orientation arrows match the physical conveyor flow (right-to-left material progression).
Chapter 04

Step-Distance & Optical Calibration

Calibrate hardware-to-software feed ratios to eliminate dimensional compression along the conveyor indexing axis:

  1. Place flat test material onto the belt and focus using the automated dual-dot optical focus routine.
  2. Navigate to Settings → Accessory → Conveyor → Step Calibration. Burn the standard 100.00 mm calibration marks.
  3. Measure the center-to-center distance using digital vernier calipers. Enter the observed value into XCS to auto-adjust the stepper scale.

Interactive Calibration Scale Tool

Input nominal settings and your actual measured caliper length to compute the corrected XCS factor:

Chapter 05

Batch Processing & Large Materials (≤ 500 mm)

The Auto Streamline™ Conveyor executes both discrete batch arrays and oversized continuous pass-through jobs:

  • Batch Staging: Scatter identical blanks on the belt without contact or overlap Quick Start Guide: P. 09"Ensure that you use identical materials... Ensure that the materials do not touch or overlap with each other." .
  • Smart-Fill Matching: Position artwork on master part; click Smart Fill to duplicate across all detected blanks automatically.
  • Large Materials (≤ 500 mm) Central Line Rule: When processing large materials up to 500 mm, laser beams are directed solely onto the conveyor central line. Any portion of material to the left of this line will not be processed Quick Start Guide: P. 10"When processing large materials, the device directs laser beams solely onto the central line of the conveyor... any portion to the left of this central line will not be processed." .
  • Continuous Processing: Click Process → Start to execute marking, auto-indexing, and continuous part ejection.
Operator Knowledge Verification

xTool Conveyor Diagnostic & Troubleshooting Assessment

Test everything covered above: conveyor history, geometries, drive motors and motion control, safety baselines, hardware docking, XCS configuration, step calibration, and batch / large-material processing. Select an answer to see its explanation.

Let's talk

Open to automation, controls, and industrial engineering roles and internships.