Detroit, Michigan SYSTEM ONLINE

Building the logic that runs
the assembly line.

I'm an Industrial Engineering student at Wayne State University and an automation engineer who programs the PLCs, HMIs, and inspection systems that keep automotive production lines running — and catches the failures that shouldn't reach the next station.

2+ Years of hands-on PLC, HMI & vision commissioning
Focus
Automation & controls
Program
B.S. Industrial Engineering, exp. 2027
Certifications
Six Sigma Green Belt GCCH-1 GCCS-2

Experience

Three roles, three different floors — a control room, a courtside, and a lumber yard.

  1. Jan 2023 – Aug 2023  ·  May 2024 – May 2025  ·  May 2026 – Aug 2026

    Automation Engineer

    Control System Integrators — Lansing, MI

    • Programmed PLC logic and HMIs for automotive-industry projects with customers including GM Toledo and GM LDT.
    • Built new inspection logic for a camera system at GM Lansing Delta Township to raise failure detection on final vehicle assembly.
    • Commissioned the AMR traffic system at GM Toledo, coordinating autonomous mobile robots that transport transmissions through truck and van manufacturing.
    Studio 5000 TIA Portal FTView PLC / HMI
  2. Aug 2019 – Oct 2019

    Boys Freshman JV Tennis Coach

    Northville High School — Northville, MI

    • Coached a freshman tennis team through practices and matches against nearby schools.
    • Led practices as lead instructor and built a team-first culture for first-year players.
  3. May 2021 – Jun 2021

    Forklift Driver

    Guthrie Lumber Company — Livonia, MI

    • Packaged customer orders for delivery trucks and kept the yard organized.
    • Operated a forklift to fill orders on time and keep material moving to schedule.

Education

Wayne State University

Bachelor of Science, Industrial Engineering

Expected graduation: May 2027

Completed coursework

  • Quality Control
  • Engineering Economy
  • Work Design
  • Six Sigma
  • Systems Simulation

Current coursework

  • Engineering Capstone
  • Digital Automation
  • Operations Research
  • Data Science & Analysis
  • Systems Engineering

Skills

Programming

  • Python
  • MATLAB
  • C++

Controls & automation

  • Studio 5000
  • TIA Portal
  • FTView

Certifications

  • Six Sigma Green Belt
  • GCCH-1
  • GCCS-2

About Me

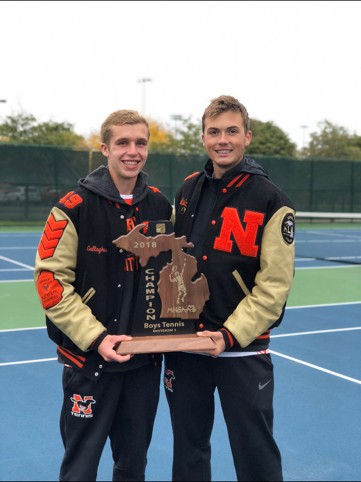
Ilija and a teammate holding the 2018 Michigan Division 1 boys tennis championship trophy

I love to get outside and play tennis or basketball. I also am an avid reader and like to catch a local play or musical. I also like board games like Settlers of Catan and getting together with family.

Technical SOP & Subject Matter Guide

xTool Auto Streamline™ Conveyor

Interactive mechanical integration, precision calibration, batch vision automation, and diagnostics calibrated to the official xTool Quick Start Guide. Hover over any step or citation badge to inspect physical dynamics.

Chapter 01

Safety & Operational Baselines

Operating a continuous auto-streamline conveyor involves strict adherence to optical enclosure thresholds and hand-clearance zones:

  • Enclosure Shield Height (≤ 5 mm): Pull down the protective enclosure until it rests no more than 5 mm above the material before running Quick Start Guide: P. 09 & 10"Pull down the protective enclosure until it remains no more than 5 mm above the material before processing." .
  • E-Stop Unobstructed Reach: Maintain unobstructed physical line-of-sight and immediate reach to the F1 Ultra red emergency stop mushroom button at all times.
  • Active Processing Zone Safety: When placing materials during processing, keep hands away from the central laser processing area to avoid skin injuries Quick Start Guide: P. 09"When placing materials during processing, keep your hand away from the processing area to avoid skin injuries." .
  • Substrate Boundary Rule: Ensure all workpieces are identical and strictly do not touch or overlap with each other on the belt surface Quick Start Guide: P. 09"Ensure that you use identical materials... Ensure that the materials do not touch or overlap with each other." .
Chapter 02

Hardware Docking (F1 Ultra Fastening Kit)

The F1 Ultra utilizes a dedicated fastening kit distinct from the F2 Ultra Quick Start Guide: P. 01"xTool F1 Ultra fastening kit: Fastening piece A, Fastening piece B, Screw M4*10, Screwdriver 3 mm." . Follow the 4-step mechanical docking sequence:

Step 1

Mount Piece B

Fasten Piece B to conveyor using two M4*10 screws and 3 mm driver. Verify correct bracket orientation Quick Start Guide: P. 06"Place fastening piece B in the correct direction. Fastening piece B, Screw M4*10, Screwdriver 3 mm." .

Step 2

Mount Piece A

Attach Piece A to F1 Ultra base plate using two M4*10 screws and 3 mm driver Quick Start Guide: P. 07"xTool F1 Ultra, Fastening piece A, Screw M4*10, Screwdriver 3 mm." .

Step 3

Align & Join

Align the holes on Fastening Pieces A and B; secure together with two M4*10 screws Quick Start Guide: P. 07"Align the holes on the two fastening pieces... Screw M4*10, Screwdriver 3 mm." .

Step 4

Cable Interface

Plug 90° elbow connection cable between conveyor side port and F1 Ultra rear connector Quick Start Guide: P. 08"Connection cable plugged into side of conveyor and peripheral port of F1 Ultra." .

Chapter 03

Software Configuration (XCS)

Synchronize stepper motor index pulses with xTool Creative Space (XCS) to control workpiece progression:

  1. Connect F1 Ultra via USB-C or local Wi-Fi and verify the device dashboard indicates Connected.
  2. Open Device Settings (Gear Icon) adjacent to the F1 Ultra device card in XCS.
  3. Under Working Mode, switch from Regular Surface to Conveyor (select Auto-Stream or Long Material).
  4. Verify software feed vector orientation arrows match the physical conveyor flow (right-to-left material progression).
Chapter 04

Step-Distance & Optical Calibration

Calibrate hardware-to-software feed ratios to eliminate dimensional compression along the conveyor indexing axis:

  1. Place flat test material onto the belt and focus using the automated dual-dot optical focus routine.
  2. Navigate to Settings → Accessory → Conveyor → Step Calibration. Burn the standard 100.00 mm calibration marks.
  3. Measure the center-to-center distance using digital vernier calipers. Enter the observed value into XCS to auto-adjust the stepper scale.

Interactive Calibration Scale Tool

Input nominal settings and your actual measured caliper length to compute the corrected XCS factor:

Chapter 05

Batch Processing & Large Materials (≤ 500 mm)

The Auto Streamline™ Conveyor executes both discrete batch arrays and oversized continuous pass-through jobs:

  • Batch Staging: Scatter identical blanks on the belt without contact or overlap Quick Start Guide: P. 09"Ensure that you use identical materials... Ensure that the materials do not touch or overlap with each other." .
  • Smart-Fill Matching: Position artwork on master part; click Smart Fill to duplicate across all detected blanks automatically.
  • Large Materials (≤ 500 mm) Central Line Rule: When processing large materials up to 500 mm, laser beams are directed solely onto the conveyor central line. Any portion of material to the left of this line will not be processed Quick Start Guide: P. 10"When processing large materials, the device directs laser beams solely onto the central line of the conveyor... any portion to the left of this central line will not be processed." .
  • Continuous Processing: Click Process → Start to execute marking, auto-indexing, and continuous part ejection.
Operator Knowledge Verification

Conveyor Diagnostic & Troubleshooting Assessment

Test your operational problem-solving skills across hardware mounting, enclosure clearance, and large material processing rules.

Let's talk

Open to automation, controls, and industrial engineering roles and internships.